Our products for high-purity sodium silicate industries
To empower global industries with high-purity industrial silicate solutions through manufacturing excellence, reliable supply chains, and a steadfast commitment to technical innovation and customer success.
Our Vision
To be the world’s most trusted partner in industrial chemistry, recognized for our legacy of quality, integrity, and sustainable manufacturing practices that drive the next generation of industrial growth.
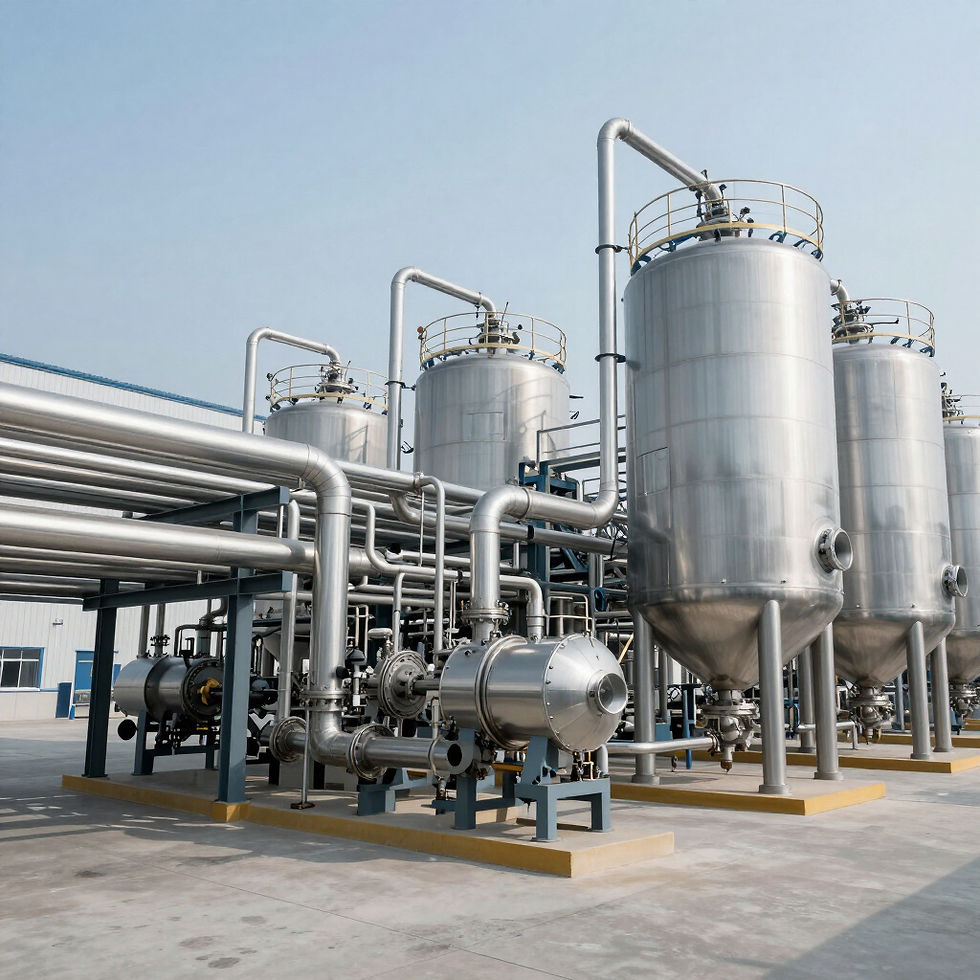
Our Strategic Manufacturing Process
01
Raw Material Selection
Sourcing high-purity sand and soda ash to initiate the silicate synthesis.
02
Furnace Charging
Controlled mixing and feeding of materials into industrial-grade furnaces.
03
High-Temp Melting
Thermal processing at 1400°C for optimal chemical bonding.
04
Cooling & Solidification
Controlled cooling to produce glass lumps with desired properties.
05
Industrial Crushing
Precision milling ensuring uniform particle size for industrial use.
06
Liquid Dissolution
Steam digestion creating specific concentration silicate liquids.
07
Advanced Filtration
Rigorous filtration ensuring consistent high-grade industrial purity.
08
Quality Inspection
Batch-wise testing ensuring adherence to global ISO standards.
DETERGENTS
WATER TREATMENT
Industries We Serve
Providing specialized silicate solutions for major industrial sectors globally.
FOUNDRY
SILICA GEL
CONSTRUCTION
CERAMICS
PAPER
MINING
TEXTILE
CHEMICALS
Our Products
Comprehensive range of high-purity industrial silicate and silica solutions.
Sodium Silicate Glass
High-purity soluble glass used in detergent, textile, and chemical sectors.
Sodium Silicate Liquid
Premium grade liquid concentrate for construction chemicals and paper industries.
Sodium Silicate Powder
Specialized anhydrous powder for precise industrial applications and welding.
Why Choose LJ Industries
Premium Quality
Modern Manufacturing
Bulk Production
Custom Specifications
Utilizing high-purity raw materials and advanced synthesis to ensure every batch meets rigid international standards.
ISO-certified facilities with automated production lines guarantee uniform physical and chemical properties.
Scalable infrastructure supporting high-volume supply chain needs for massive industrial operations.
Tailored SiO₂/Na₂O ratios engineered to meet your unique industrial formulation requirements perfectly.
Export Ready
Technical Support
Timely Delivery
Global Supply
Supplying major industrial hubs across six continents with a robust global export framework.
Access specialized technical assistance and chemical consultancy from our expert laboratory team.
Strategic logistics network guaranteeing strictly on-time delivery across domestic and international markets.
Connecting our Rajasthan and Gujarat manufacturing units to global markets with excellence.